
In the majority of die failures, cracking is only the final visible symptom — the root cause lies in repeated thermal cycling damage.
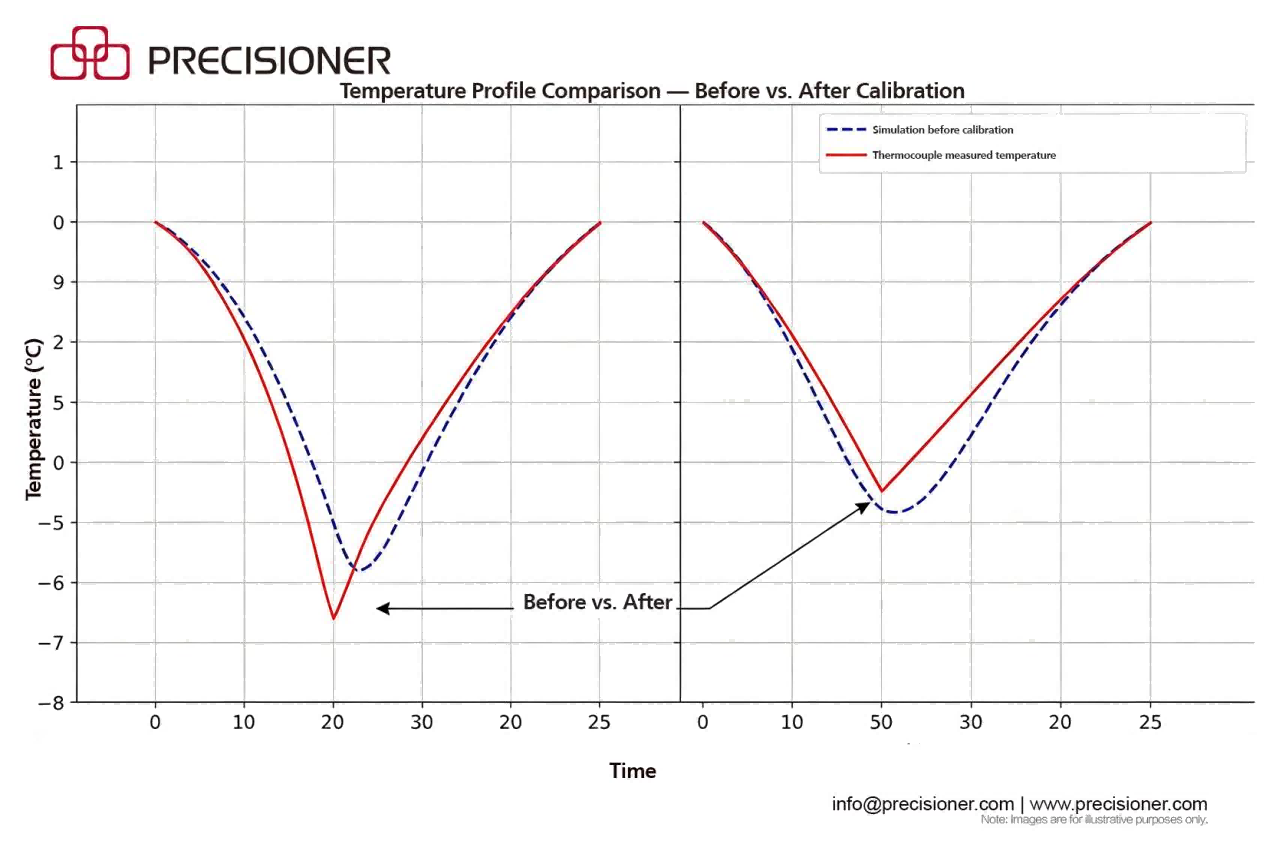
Figure 1 — Thermal Cycle Curve
In the hundreds of die projects we have been involved with in recent years, cooling channels are most often laid out in straight lines, prioritizing the easiest drilling paths and bypassing structurally complex areas such as slides and inserts — not because those areas do not need cooling, but because drilling there is inconvenient. The cooling system is treated as an afterthought rather than a design starting point. The result: hot spots accumulate, die wear accelerates, and quality defects — shrinkage porosity, die soldering, flash, and others — ultimately emerge.
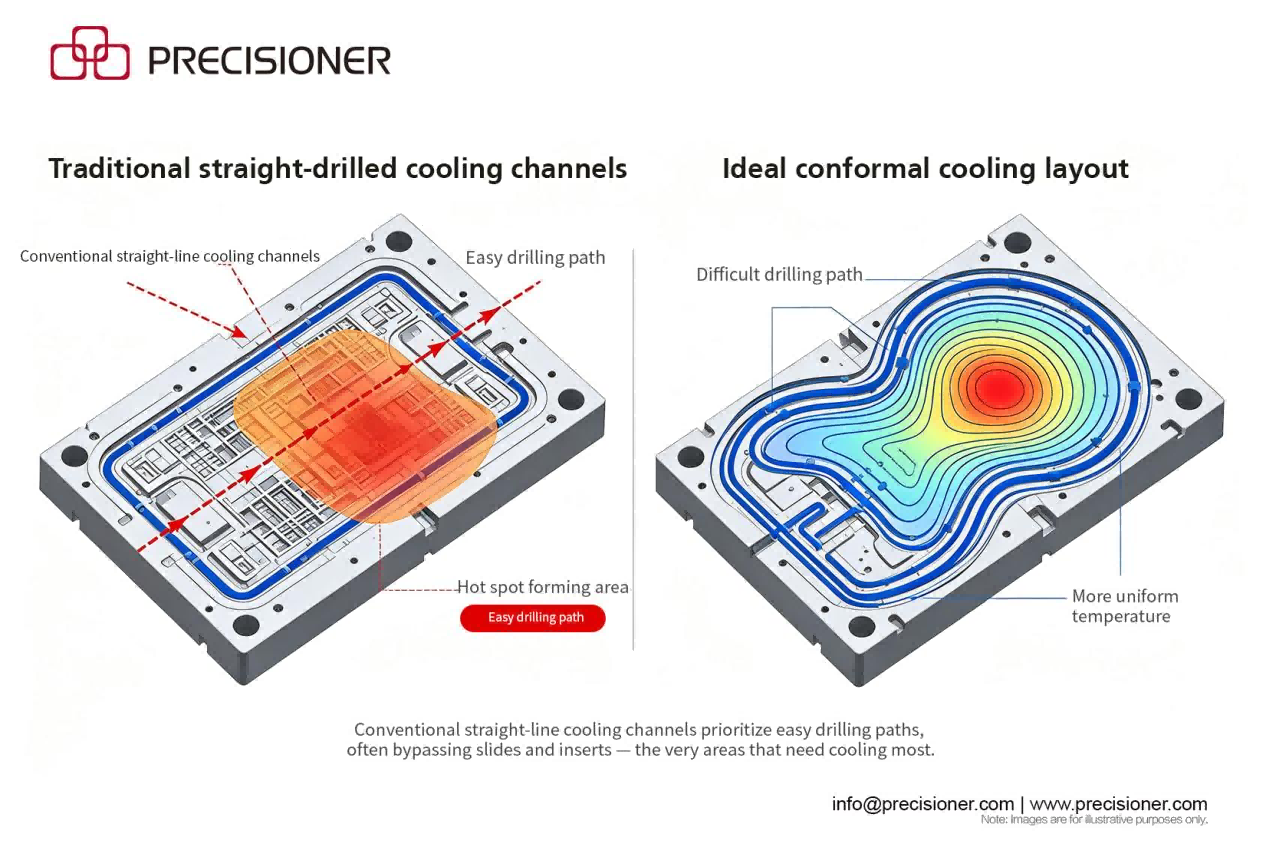
Traditional straight-drilled cooling channels (left) vs. ideal conformal cooling layout (right). Conventional straight channels prioritize the easiest drilling paths and often bypass slides and inserts — precisely the areas that need cooling the most.
The data: The Cost of Poor Cooling Design
Drawing on die production data accumulated over years of mass production at Precisioner, we have distilled several clear facts that directly determine casting yield rate and die life.
· Uneven cooling is not just a temperature issue — it is a common root cause of multiple defect types. Die soldering, cold shuts, flash, and thermal fatigue in the die — trace them back to the source, and they often point to the same problem: non-uniform heat distribution.
· Among the large-scale die casting enterprises we work with, projects that bring cooling channel design forward to the die structure definition stage show significantly better die life and yield performance than projects where cooling channels are added only after the part geometry is finalized.
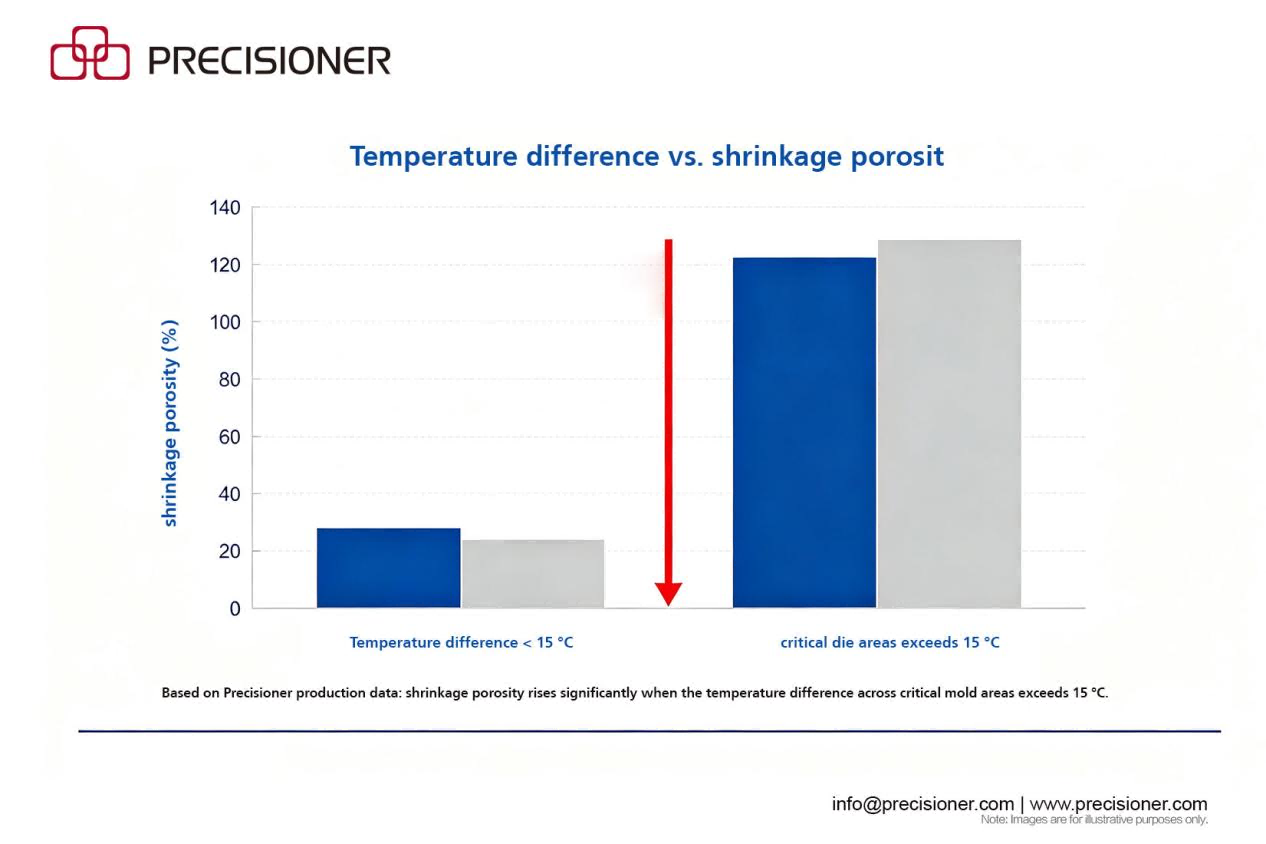
Figure 3 — Temperature Difference vs. Porosity
An Industry Shift Underway
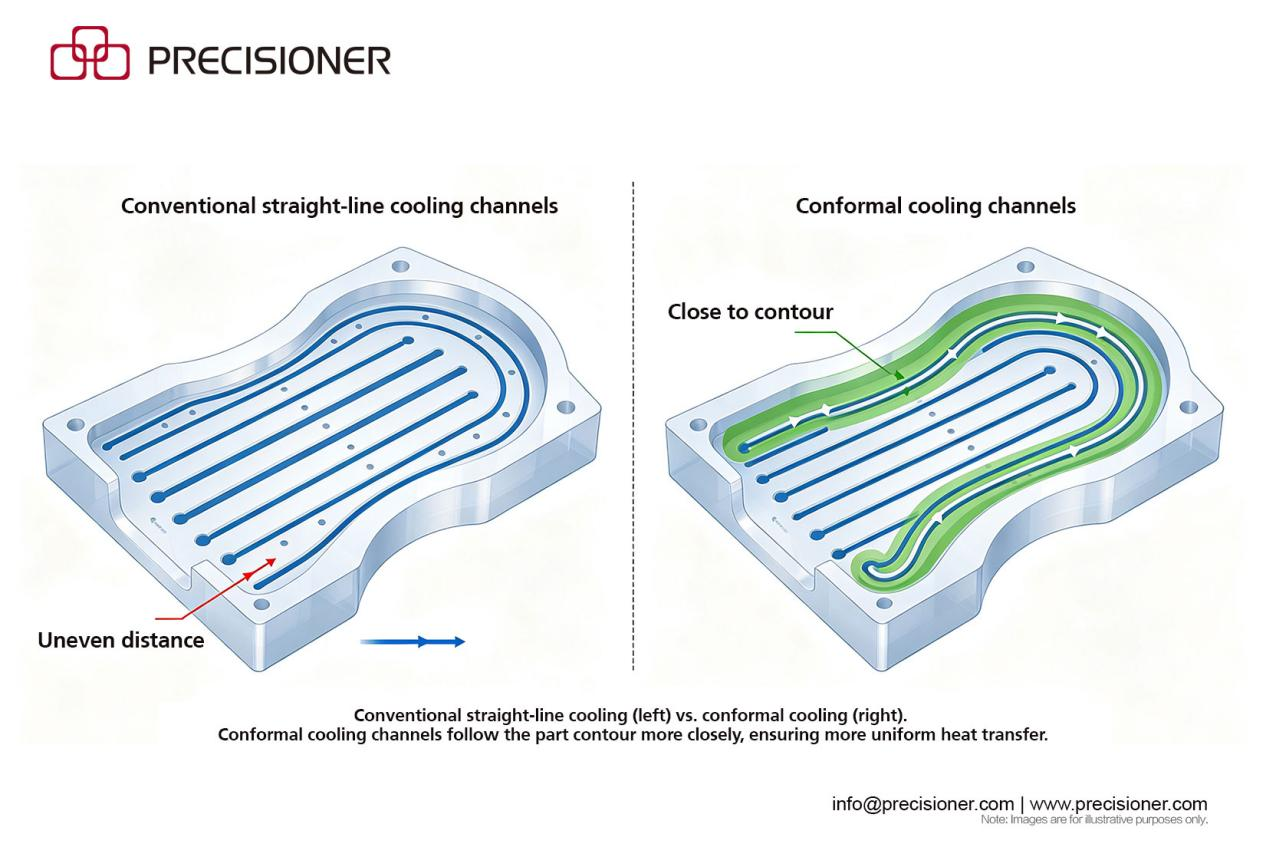
Conformal cooling has evolved from a niche technology in its early days to a mainstream engineering solution. Enabled by additive manufacturing, cooling channels can now be positioned precisely along contours that closely follow the part geometry — targeting the areas that require the most thermal control. Compared to traditional straight-drilled channels, conformal cooling has demonstrated clear advantages in reducing cooling cycle time and extending die life, validated in extensive mass production practice — particularly on complex, thin-walled components, where the benefits are especially pronounced. Today, this technology is shifting from a "nice-to-have" to a "must-have" in an increasing number of die casting projects.
What We Have Done: Empirical Calibration of the Interfacial Heat Transfer Coefficient (IHTC)
This is Precisioner's core capability in the field of thermal management.
In die casting simulation, the Interfacial Heat Transfer Coefficient (IHTC) between the casting and the die is the single most influential parameter determining the accuracy of thermal simulation. Yet the vast majority of simulations rely directly on software default values. After testing IHTC across more than a hundred dies under real production conditions, we found that the deviation between software default parameters and measured values exceeds 50% under multiple process conditions. This means that for a large number of dies relying on default parameters for flow analysis, the cooling predictions deviate significantly from actual heat transfer efficiency. Quality problems often remain hidden within that gap.
By feeding measured IHTC data back into simulation models, Precisioner is building a closed-loop verification system of "simulation → die trial → empirical calibration → re-simulation" — rather than stopping at the stage of "the simulation says it's fine."
Key Takeaway
If shrinkage porosity, die soldering, or short die life have been persistently affecting your production line, we recommend starting with the cooling system. Before looking into alloy composition or die casting machine parameters, examine your thermal management approach first — more often than not, the answer lies in the cooling channels.
If you have technical questions about thermal management, or would like to learn more about Precisioner's cooling design methodology and IHTC measurement capabilities, we welcome you to connect with our engineering team.
If you are facing technical challenges with thermal management or mold life, we welcome you to reach out. We can check whether our IHTC database already has a proven solution applicable to your process conditions.
--- Precisioner Engineering Team